Aluminum Log Furnace
Multi-Log Furnace with Hot Shear or Hot Saw
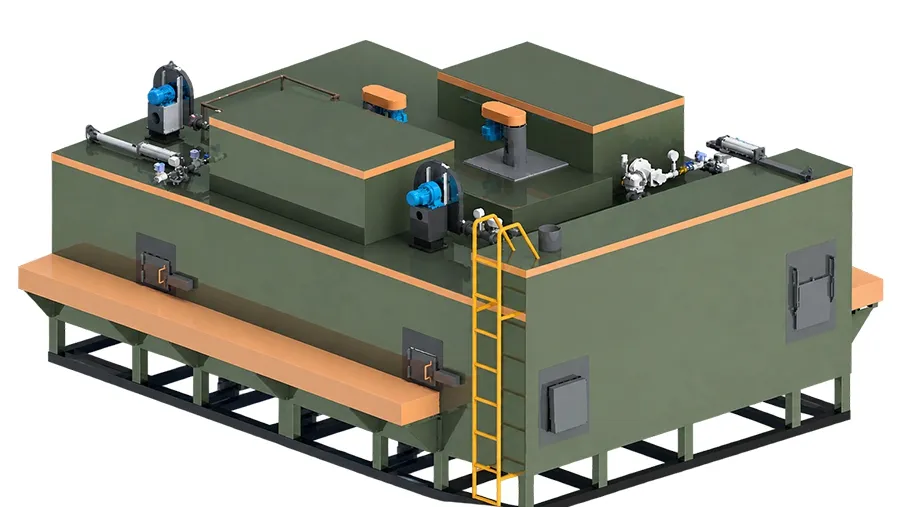
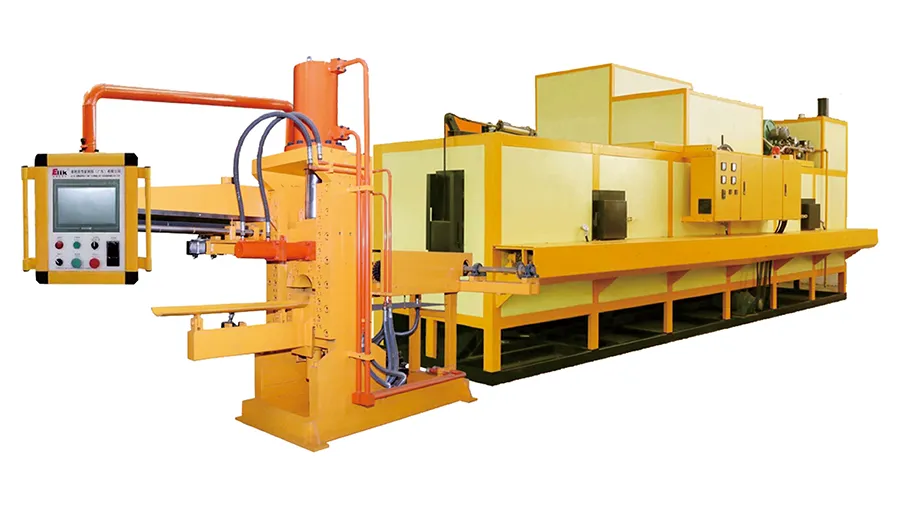
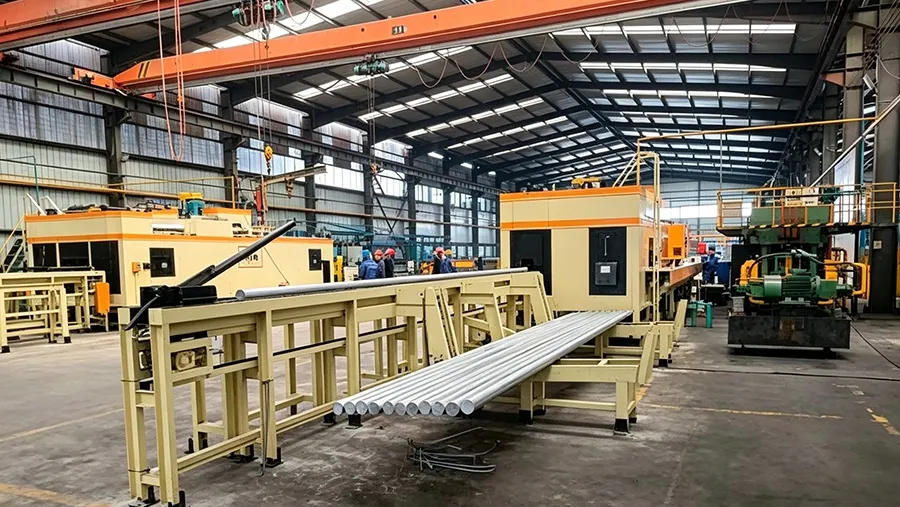
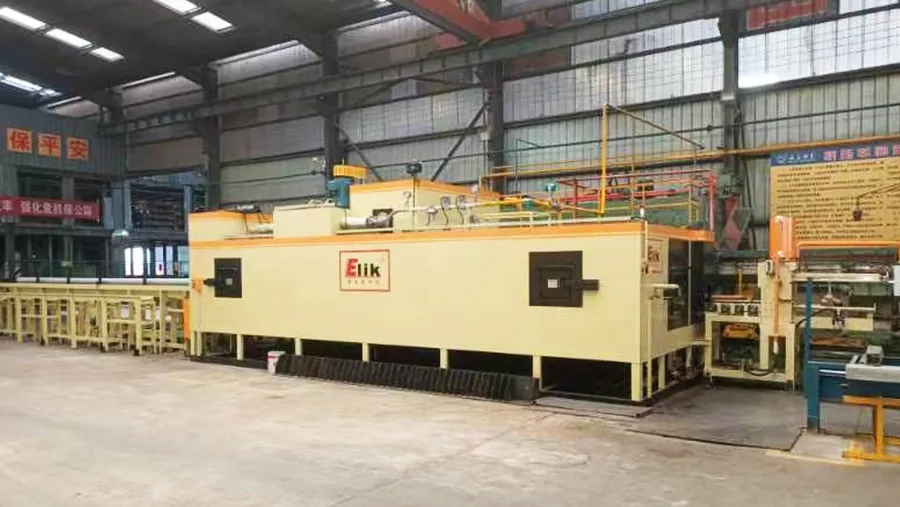
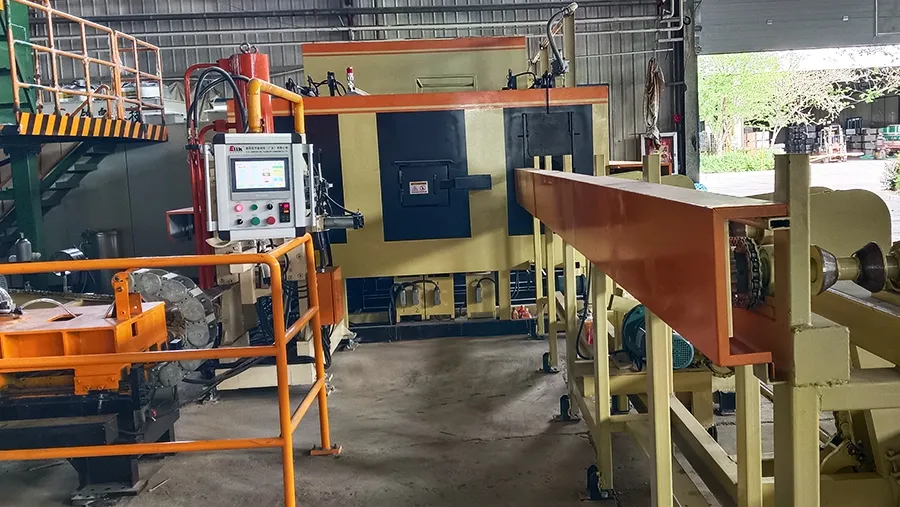
The ELIK multi-log furnace simultaneously heats multiple long aluminum logs prior to extrusion, and it is paired with an automatic hot shear or hot saw to cut the logs into the required billet lengths. Intended for high-tonnage presses that operate at high-speed cycle rates, it provides a continuous stream of billets at standard extrusion temperature to ensure that large presses are fed without interruption.
Automatic hot shear or hot saw, timed lubrication, a precision electronic control system, hydraulics, cooling, an intelligent circulation heating system, storage and in/out feed conveyors and a waste-heat exchange system are all integrated into a single unit in the furnace.
| Press tonnage | Log diameter (mm) | Pre-heat time (h) | Extrusion cycle (s/log) | Log temp. difference (°C) | Energy (m³/t Al) | Total power (kW) |
| 600T- 1450T | Ø80-Ø152 | 2.5~3 | 90 | ≦±5 | 20 | 15~30 |
| 1650T-2000T | Ø178-Ø203 | 3.5~4 | 90 | ≦±5 | 20 | 35~55 |
| 2400T-3600T | Ø228-Ø320 | 4.5~5 | 120 | ≦±5 | 20 | 45~70 |
| 4000T-7000T | Ø330-Ø406 | 5.5~6 | 120 | ≦±5 | 20 | 70~100 |
| 8000T-10000T | Ø418-Ø600 | 6.5~8 | 150 | ≦±5 | 20 | 100~150 |
- Proportional precision combustion
PLC closed-loop control with proportional valves regulates fire rate and air-fuel ratio based on temperature requirements, maintaining a controlled combustion state and achieving ±4°C log temperature consistency. - Flue-gas heat recovery
A waste-heat recovery system pre-heats combustion air to roughly 300 degrees Celsius, preventing cold air from entering the chamber directly and significantly reducing thermal loss. - Fully sealed, reinforced insulation
The chamber is all-stainless, welded in one piece, with a closed-box roof design and a thickened insulation layer to reduce heat loss from the furnace chamber. - Gravity roll-feed system
A simplified furnace-bottom push-feed structure mechanically advances logs based on their own weight and track slope, resulting in a solid, reliable conveying operation with fewer moving parts. - High-strength anti-deformation log rack
A high-strength, single-weldment log storage rack replaces typical rail steel, resisting high-temperature deformation and lowering the possibility of log jams or sticking. - Independent dual-zone control
The chamber is divided into two zones: pre-heat and soak/uniform-temperature, which are independently controlled to allow for stepwise heating and more even log temperature distribution.
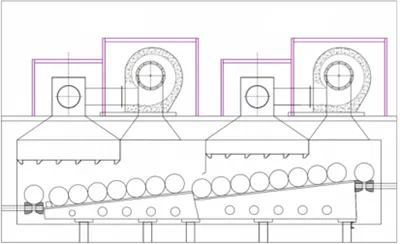
The furnace chamber accommodates over a dozen logs simultaneously, each of which is in a distinct heating phase. The logs are advanced through pre-heating and constant-temperature soaking stages by a continuous-push mechanism, which discharges billets at standard extrusion temperature in conjunction with the high-speed cycle of the press. The cutting process is conducted in a consistent manner using either a fully automatic hydraulic hot shear or a fully automatic hot saw.
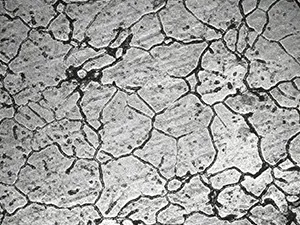
- The actual billet temperature is precisely controlled throughout the cycle.
- The PLC touchscreen control is fully automated and has the ability to record and recognise the heating time, temperature, and billet alloy. It can also select the billet.
- From the infeed and discharge of the billet to the opening of the extrusion press feed, the operation is entirely automated.